

Metalworking Fluid Water Quality: Diagnose Before Changing Oil
Foam, deposits or corrosion in a water-miscible metalworking fluid do not identify one cause. Replacing the concentrate before separating incoming-water quality from the condition of the working sump can simply repeat the problem. The useful first decision is which sample to coll
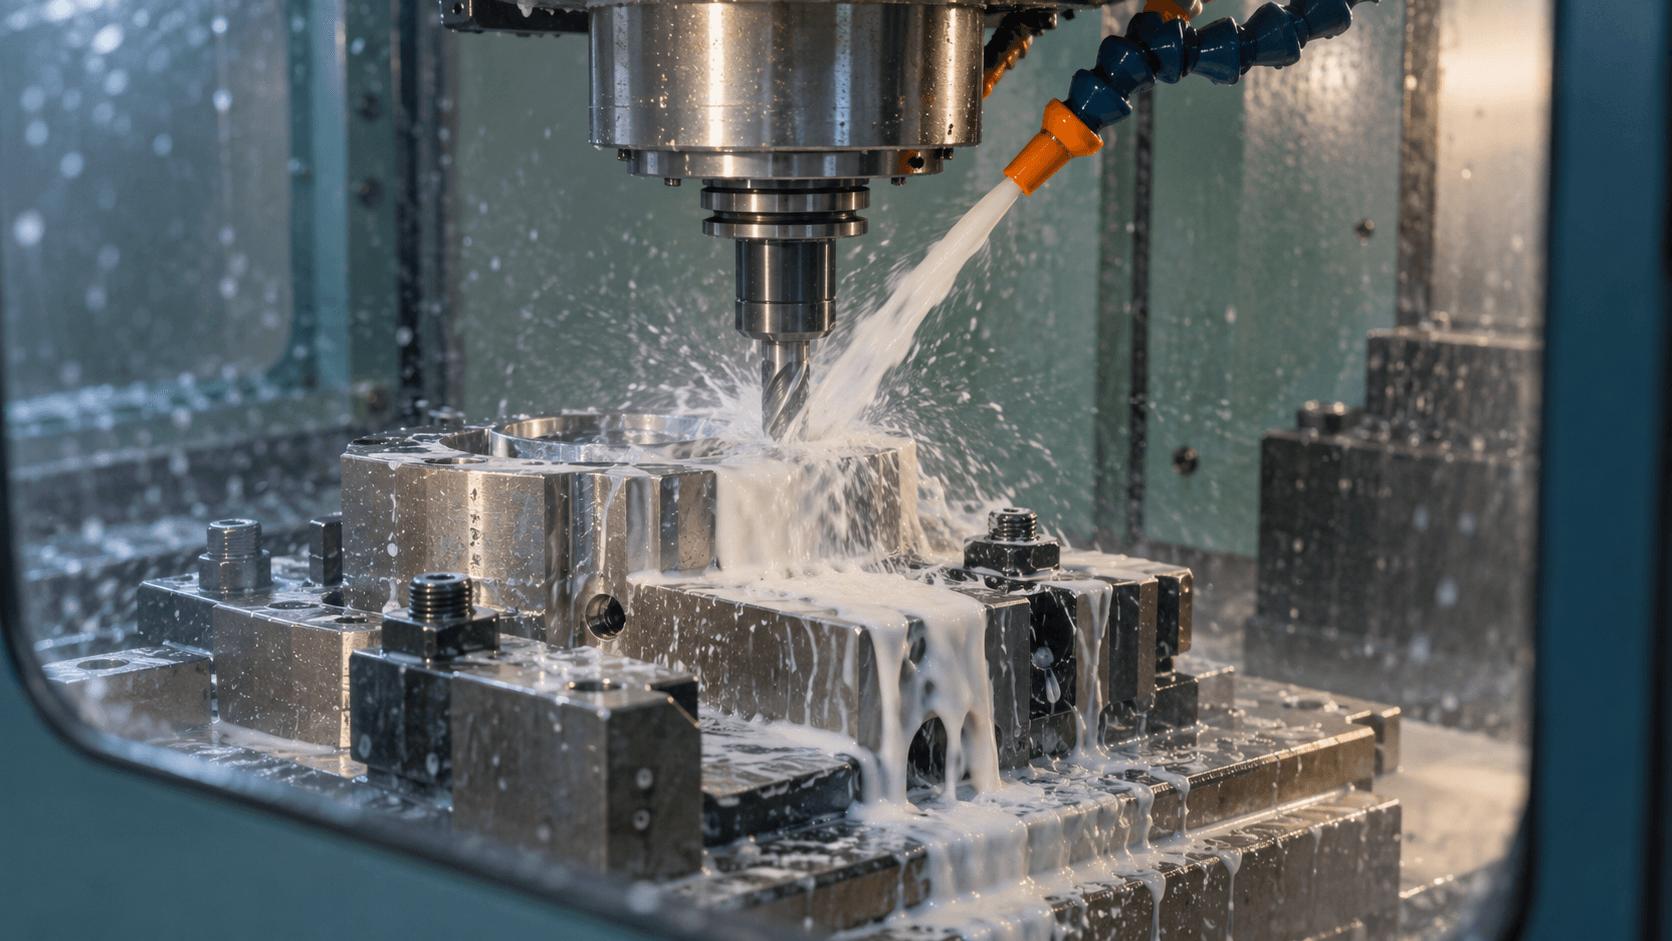
Foam, deposits or corrosion in a water-miscible metalworking fluid do not identify one cause. Replacing the concentrate before separating incoming-water quality from the condition of the working sump can simply repeat the problem. The useful first decision is which sample to collect and which variable to hold constant.
Sample incoming water separately from the working sump
Collect the water actually used for a new charge and top-ups, not merely the water described on an old municipal report. If the plant treats or blends water, identify the sampling point and record the treatment route. Collect a separate representative working-fluid sample under the agreed plant procedure, noting fluid identity, concentration, age, top-up history and contamination.
Evaporation removes water while dissolved salts can remain; continuing top-ups can therefore change the sump's ionic composition. A fresh dilution made with incoming water cannot by itself diagnose an aged bath. Conversely, a problem in an aged sump does not prove that the incoming water is unsuitable. Supplier guidance from Quaker Houghton treats water quality as an ongoing variable, while HSE MW5 addresses management of the working metalworking fluid. These are related but different tasks.
Hardness does not measure every water-related risk
Hardness mainly characterizes calcium and magnesium. Chloride, conductivity and microbiological condition answer different questions. Water that meets a hardness target may still need review for other constituents; conductivity alone does not identify which ions are present.
No single hardness limit applies to every coolant. The MOS emulsifiable metalworking coolant family contains multiple grades, but its imported parameter rows do not unambiguously map every test value to every grade. Do not turn those rows into a universal hardness, corrosion-test or working-concentration promise. The semi-synthetic cutting-fluid family is a separate candidate, not proof that it tolerates the same water.
| Finding | Prioritize checking | Do not conclude yet |
|---|---|---|
| Foam rises after a change | Concentration, water treatment, agitation and air ingress | That low hardness is the sole cause |
| Deposits or poor emulsion stability | Water chemistry, dilution procedure and exact concentrate | That every soluble oil is incompatible |
| Corrosion appears | Chloride and other water data, fluid concentration, metal and contamination | That a hardness measurement proves the cause |
| Conductivity rises during service | Evaporation, top-ups, contamination and other analytical results | That the fresh-water supply alone changed |
Run a reference-water comparison before blaming the coolant
Prepare two fresh dilutions of the same concentrate: one with supplier-agreed reference water and one with the actual plant water. Use the same verified concentration, addition order, mixing procedure, vessels and hold conditions. Follow the grade's handling instructions; do not mix concentrate families as an informal remedy.
Record appearance and separation, foam under a defined repeatable agitation, and relevant deposit or metal-compatibility observations. Keep the working-sump sample separate. If the plant-water dilution behaves differently while the reference is satisfactory, investigate water–grade compatibility. That supports a focused next test; it does not isolate chloride, hardness or a particular additive without further analysis.
If both fresh samples are satisfactory but the sump is not, investigate service concentration, contamination, treatment history and operating conditions before changing the purchased grade. A small fresh-dilution trial cannot prove cutting performance, tool life or long-term fluid stability. Qualified plant personnel should assess the actual machine trial and fluid-management requirements.
Turn the result into a grade-specific coolant enquiry
Send the machining process and metals, machine and delivery method, current coolant identity and concentration, incoming-water analysis with sampling date and point, treatment route, sump history and the observed symptom. Include the reference-versus-plant-water comparison, relevant sample quantities, order volume, packaging and destination.
Use the emulsifiable coolant enquiry page to request a specific grade, its recommended water envelope and dilution procedure, current TDS/SDS and an agreed trial plan. This makes a quotation comparable without promising that a catalogue family will solve every foam or corrosion problem.
References: HSE MW5 and Quaker Houghton on ongoing water-quality management. Their guidance is context, not a MOS grade specification or substitute for the plant's responsible fluid-management procedure.